FANUC Series 0i-MODEL F Plus. CONNECTION MANUAL (FUNCTION) — page 208
10. SPINDLE SPEED FUNCTION
B-64693EN-1/01
- 1618 -
3741
Maximum spindle speed for gear 1
3742
Maximum spindle speed for gear 2
3743
Maximum spindle speed for gear 3
3744
Maximum spindle speed for gear 4
[Input type] Parameter input
[Data type] 2-word spindle
[Unit of data] min
-1
[Valid data range] 0 to 99999999
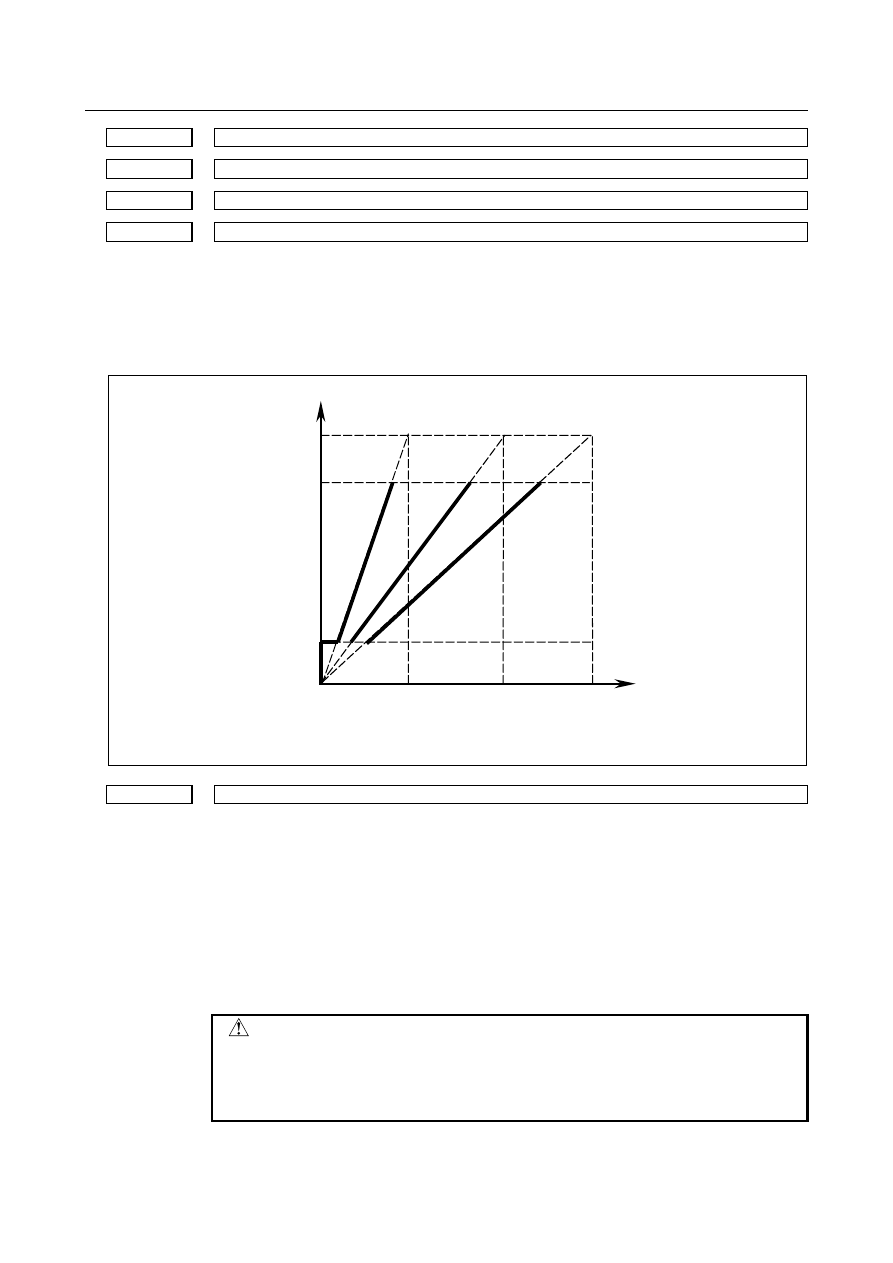
Set the maximum spindle speed corresponding to each gear.
Spindle motor max. clamp speed
(Parameter No.3736)
Spindle speed command
(S command)
Max. speed (4095, 10V)
Spindle motor minimum clamp speed
(Parameter No.3735)
Spindle motor speed
Gear 1
Max. speed
(Parameter
No.3741)
Gear 2
Max. speed
(Parameter
No.3742)
Gear 3
Max. speed
(Parameter
No.3743)
3772
Maximum spindle speed
[Input type] Parameter input
[Data type] 2-word spindle
[Unit of data] min
-1
[Valid data range] 0 to 99999999
This parameter sets the maximum spindle speed.
When a command specifying a speed exceeding the maximum speed of the spindle is
specified , or the speed of the spindle exceeds the maximum speed because of the spindle
speed override function, the spindle speed is clamped at the maximum speed set in the
parameter.
CAUTION
1 When 0 is set in this parameter, the speed of the spindle is not
clamped.
2 When spindle speed command control is applied using the PMC,
this parameter has no effect, and the spindle speed is not clamped.
B-64693EN-1/01
10. SPINDLE SPEED FUNCTION
- 1619 -
NOTE
1 For M series, this parameter is valid if the function of constant
surface speed control is enabled(bit 0(SSC) of parameter No.8133
is 1).
2 When the constant surface speed control is enabled, the spindle
speed is clamped at the maximum speed, regardless of whether
the G96 mode or G97 mode is specified.
3775
Default P command value for spindle selection in multi-spindle control
NOTE
When this parameter is set, the power must be turned off before
operation is continued.
[Input type] Parameter input
[Data type] Word path
[Valid data range] 0 to 32767
When bit 3 (MPP) of parameter No. 3703 is set to 1 and bit 2 (MPA) of parameter No.
3706 is set to 1 in multi-spindle control, set a default P command value applicable if S_P_
is not specified even once after power-up.
3781
P code for selecting the spindle in multi-spindle control
[Input type] Parameter input
[Data type] Word spindle
[Valid data range] 0 to 32767
If bit 3 (MPP) of parameter No. 3703 is set to 1, set the P code to select each spindle
under multi-spindle control. Specify the P code in a block containing the S command.
[Example] If the P code value for selecting the second spindle is set to 2,
S1000 P2;
causes the second spindle to rotate at S1000.
NOTE
1 This parameter is valid if bit 3 (MPP) of parameter No. 3703 is set
to 1.
2 If this parameter is set to 0, the corresponding spindle cannot be
selected by a P code.
3 Under multi-path control, the P code specified here is valid for each
path.
For instance, if the P code to select the first spindle of path 2 is set
to 21, specifying S1000 P21; in path 1 causes the first spindle of
path 2 to be rotated at S1000.
4 Identical P code values cannot be used for different spindles.
(Identical P code values cannot be used even if the paths are
different.)
5 When this parameter is used (when bit 3 (MPP) of parameter No.
3703 is set to 1), the spindle command selection signal is invalid.
6 To use this parameter, enable the multi-spindle control function(bit
1(MSP) of parameter No.8133 is 1).
10. SPINDLE SPEED FUNCTION
B-64693EN-1/01
- 1620 -
#7
#6
#5
#4
#3
#2
#1
#0
3786
MPF
[Input type] Parameter input
[Data type] Bit
NOTE
When this parameter is set, the power must be turned off before
operation is continued.
#2 MPF
When M03/M04/M05 is commanded by "M_P_" format in multi-spindle control,
multi-spindle address P signal <Fn160-Fn161> is:
0:
Not output.
1:
Output.
NOTE
This parameter is valid when bit 3 (MPP) of parameter No.3703 is
set to 1.
#7
#6
#5
#4
#3
#2
#1
#0
3798
ESN
[Input type] Parameter input
[Data type] Bit
#1 ESN
When the multi-spindle control is enabled and bit 3 (MPP) of parameter No. 3703 is set
to 1, a spindle is specified in a program by using:
0:
P command.
1:
Extended spindle name.
A spindle to be specified is selected as follows:
Bit 1 (ESN) of
parameter No. 3798
Bit 3 (MPP) of
parameter No. 3703
Selection method
0
0
Signal selection
0
1
P command (S_P_)
1
0
Signal selection
1
1
Extended spindle name
or
P command (S_P_)
NOTE
This parameter is valid when bit 0 (EEA) of parameter No. 1000 is
set to 1.
When setting this parameter to 1, set also parameter No. 3738 and
No. 3739 properly.
11090
Path number with which the rotation of each spindle is specified
[Input type] Parameter input
[Data type] Byte spindle
[Valid data range] 0 to 10
When a path is specified for spindle commands, this parameter sets a path number with
which the rotation of a spindle can be specified.
0:
Spindle commands can be issued from all paths.
B-64693EN-1/01
10. SPINDLE SPEED FUNCTION
- 1621 -
1 to 10: Spindle commands can be issued from a set path.
NOTE
1 This parameter is valid when spindle command path specification
signal SPSP<Gn536.7> is set to "1".
2 If the setting is illegal, an alarm PS5305, “ILLEGAL SPINDLE
NUMBER” is issued when a spindle command is issued from any
one of the paths.
3 This setting does not apply to spindle commands using the spindle
select signals SWS1 to SWS4<Gn027.0 to Gn027.2, Gn026.3>.
Caution
CAUTION
1 If the primary spindle stop signal *SSTP<Gn029.6> for stopping all selected
(SWS1 to SWS4) spindles’ rotation is cleared, the speed command is restored.
A spindle not selected by SWS1 to SWS4 and rotating at its previous speed,
which is stopped using its respective command *SSTP1 to *SSTP4, cannot be
restored to that speed when the signal is cleared.
2 While a function using a position coder feedback such as feed per revolution and
a threading command is being executed, avoid changing the selection of a
position coder by using position coder selection signals PC2SLC<Gn028.7> ,
PC3SLC<Gn026.0> , and PC4SLC<Gn026.1> .
3 Type A multi-spindle control differs from Type B in the relationship between the
SWS1 and SIND signals for the first spindle. In Type A, SIND functions only when
SWS1 is set to "1". In Type B, SIND functions whether SWS1 is "1" or "0"; each
spindle is selected by either of its respective SWS1 or SIND signals being set to
"1".
Note
NOTE
1 The spindle orientation signal SOR<Gn029.5>, spindle speed override signals
SOV0 to SOV7<Gn030>, and spindle stop signal *SSTP <Gn029.6> only
function for the selected spindle.
2 The multi-spindle control allows multiple position coder interfaces to be used. But
the number of actual speed indications on the CNC screen does not change.
The speed based on the feedback information of the selected position coder is
displayed.
3 An SOR command has priority over S commands and SIND-based rotation
control from the PMC, and will cause all selected spindles to perform orientation
rotation.
Alarm and message
Number
Message
Description
PS0333
TOO MANY SPINDLE
COMMANDS
Multiple spindle commands could be found in the same block in
using an expansion spindle name.
Only one spindle could be commanded in the same block.
10. SPINDLE SPEED FUNCTION
B-64693EN-1/01
- 1622 -
Number
Message
Description
PS5305
ILLEGAL SPINDLE NUMBER
In a spindle select function by address P for a multiple spindle
control,
1 Address P is not specified.
2 Parameter No. 3781 is not specified to the spindle to be
selected.
3 An illegal G code which cannot be commanded with an S_P_;
command is specified.
4 The multi-spindle control cannot be used because the bit 1
(EMS) of parameter No. 3702 is 1.
5 The spindle amplifier number of each spindle is not set in
parameter No. 3717.
6 A prohibited command for a spindle was issued (parameter
No. 11090).
7 An invalid value is set in parameter No. 11090.
SP1202
SPINDLE SELECT ERROR
In the multi-spindle control, the spindle number other than the
valid spindle number was selected by a position coder select
signal. An attempt was made to select the spindle number of the
system having no valid spindle.
B-64693EN-1/01
10. SPINDLE SPEED FUNCTION
- 1623 -
10.13
RIGID TAPPING
Overview
In a tapping cycle (Machining center system: G84/G74, Lathe system: G84/G88), synchronous control is
applied to the tapping operation of a tapping axis and the operation of the spindle.
This capability eliminates the need to use a tool such as a float tapper, thus enabling higher-speed,
higher-precision tapping.
Whether a tapping cycle is an ordinary tapping cycle or rigid tapping cycle is determined by the
miscellaneous function code for rigid tapping M29. (A different M code can be used by setting the
parameters accordingly, but M29 is used in the description given here.)
By setting the parameters, G codes for tapping cycles can be changed to G codes for rigid tapping only. In
this case, the CNC specifies M29 internally.
To perform rigid tapping, the following must be added to the ordinary connections:
-
Connection of a position coder to the spindles
-
Addition of a sequence to the PMC
-
Setting of related parameters
To avoid duplicate descriptions, assume the following unless noted otherwise:
G code for a tapping cycle
Machining center system
Lathe system
G84/G74
G84/G88
Gear selection method
Machining center system
Lathe system
M-type or T-type gear selection method
T-type gear selection method only
Parameters used according to the number of gear stages
No.5221 to No.5224, No.5231 to No.5234, No.5241 to No.5244,
No.5261 to No.5264, No.5271 to No.5274, No.5281 to No.5284,
No.5291 to No.5294, No.5321 to No.5324,etc.
CAUTION
1 In the text of this section, a description of up to four-step gears is provided.
Gears of four steps are used with the lathe system, but gears of up to only three
steps are used with the machining center system.
2 When M-type gear selection is used for the machining center system, the
maximum spindle speed for rigid tapping (specified with parameters Nos. 5241
to 5243) must also be set for parameter No. 5243 regardless of the number of
gear steps. (For a system having a single gear step, set the same value as that
of parameter No. 5241 for parameter No. 5243. For a system having two gear
steps, set the same value as that of parameter No. 5242 for parameter No.
5243.)
The descriptions given in this section (such as spindle gear switching and M-type/T-type) are based on
the explanation given in Section "SPINDLE SPEED CONTROL."
Refer to Section "SPINDLE SPEED CONTROL" as necessary.
-
Specification of machining center system/lathe system
The differences in the specifications for rigid tapping for the machining center system and lathe system
are described below.
10. SPINDLE SPEED FUNCTION
B-64693EN-1/01
- 1624 -
M
Rigid tapping of machining center system
The tapping cycle G84 and the reverse tapping cycle G74 can be used to specify machining center system
rigid tapping.
A drilling axis can be arbitrarily selected from the basic axes X, Y, Z, as well as axes parallel to the basic
axes, by setting the corresponding parameters accordingly (bit 0 (FXY) of parameter No. 5101).
The spindle operations of G84 and G74 are reversed with respect to each other.
T
Rigid tapping of lathe system
The face tapping cycle G84 and the side tapping cycle G88 can be used to specify lathe system rigid
tapping.
Depending on the rigid tapping command, rigid tapping can be performed along the Z-axis (when G84 is
used) or the X-axis (when G88 is used).
A reverse tapping cycle, like that supported by machining center system, is not available.
See "Rigid Tapping with Spindle of Another Path" for explanations about rigid tapping between different
paths (rigid tapping on a spindle for tool post 2 as directed by a command for tool post 1) in a multi-path
system.
-
Multi-spindle control
The relationships between rigid tapping and multi-spindle control are described below.
Without multi-spindle control
Rigid tapping can be performed with the first spindle only.
With multi-spindle control
Rigid tapping can be performed by selecting the second through fourth spindles in addition to the first
spindle.
10.13.1
Connection Among Spindle, Spindle Motor, and Position
Coder
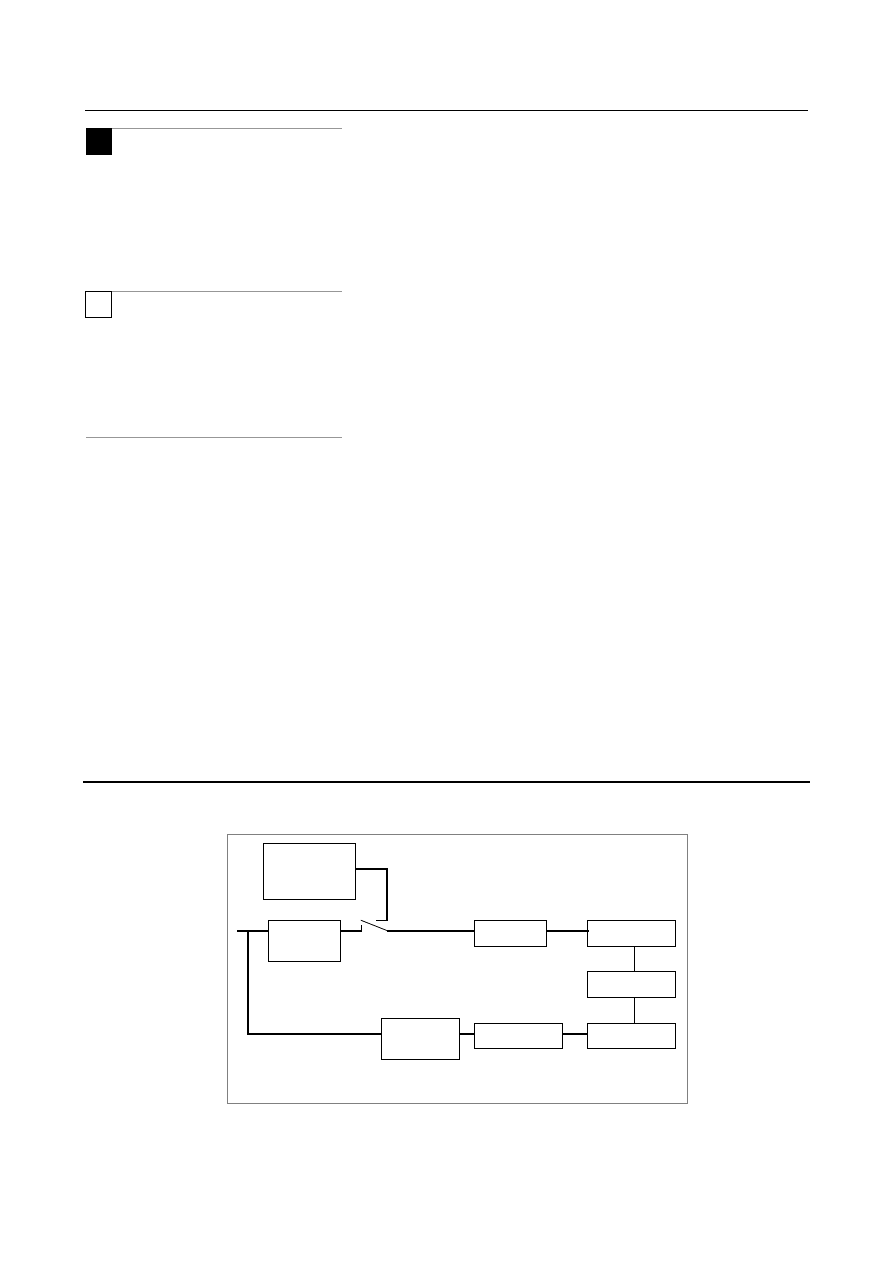
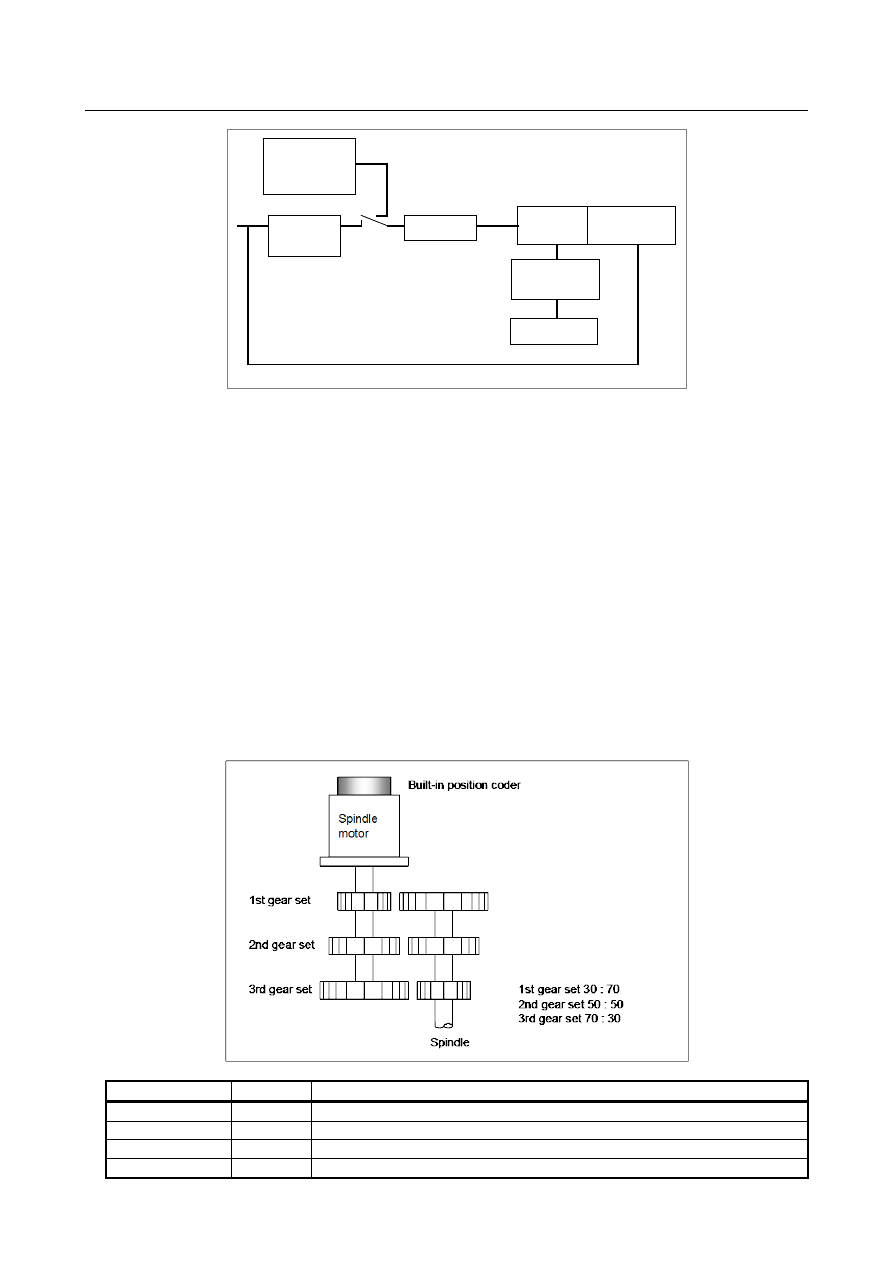
As shown in the figures (Fig. 10.13.1 (a) and Fig. 10.13.1 (b)) below a gear ratio can be inserted between
the spindle and spindle motor (n : m), and between the spindle and position coder (N : M).
Spindle control
Spindle
amplifier
Spindle motor
Spindle
Gear ratio n:m
Error counter
Gear ratio N : M
Position coder
The number of pulses per position coder revolution is set in parameter No. 3720.
Fig. 10.13.1 (a) When a position coder is externally attached (on the spindle side)
B-64693EN-1/01
10. SPINDLE SPEED FUNCTION
- 1625 -
Spindle control
Spindle
amplifier
Spindle motor
Spindle
Position coder
Error counter
Gear ratio n : m
N : M
The number of pulses per position coder revolution is
set in parameter No. 3720.
Fig. 10.13.1 (b) When a position coder is built into a spindle motor
(1) Gear between spindle and spindle motor
Up to three gear stages (machining center system) or four gear stages (lathe system) can be provided
between the spindle and the spindle motor.
The gear ratio is arbitrary. The distance of spindle rotation per revolution of spindle motor is different,
based on the gear ratio. The speed command to the spindle motor will be adjusted.
(2) Gear between spindle and position coder
The position coder is used to detect the position of the spindle.
The gear ratio between the spindle and position coder is set in parameters Nos. 5221 to 5224 and 5231 to
5234.
When a position coder is externally attached, the gear ratio between the spindle and position coder is not
changed by a gear change between the spindle motor and spindle. So, set the same number of teeth in
parameters Nos. 5221 to 5224 and 5231 to 5234.
When a position coder is built into a spindle motor, the gear ratio between the spindle and position coder
is changed by a gear change between the spindle motor and spindle. So, set the number of teeth for each
gear in parameters Nos. 5221 to 5224 and 5231 to 5234.
Example of setting for the machining center system)
Parameter No.
Set value
Meaning
5221
70
Number of teeth of the 1st gear for the spindle side
5222
50
Number of teeth of the 2nd gear for the spindle side
5223
30
Number of teeth of the 3rd gear for the spindle side
5231
30
Number of teeth of the 1st gear for the position coder side
Нет комментариевНе стесняйтесь поделиться с нами вашим ценным мнением.
Текст